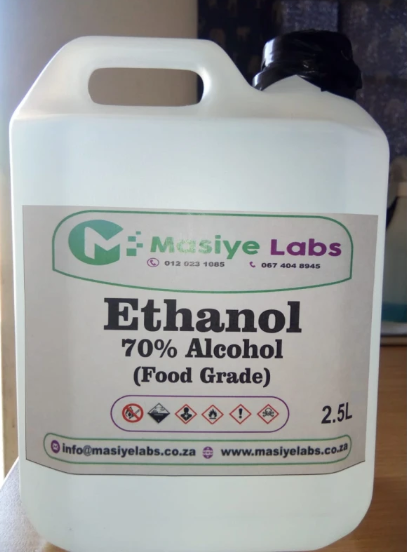
Food Grade Ethanol
High-Purity Food Grade Ethanol for Commercial Applications
Our Food Grade Ethanol is a high-purity ethanol produced and handled for applications where ethanol suitable for food and beverage processing is required. Also known as ethyl alcohol, ethanol is a versatile ingredient and processing material used in food manufacturing, flavor and extract production, beverage applications, and selected pharmaceutical and industrial processes.
Our ethanol is supplied according to agreed technical specifications and is suitable for manufacturers, food processors, beverage companies, ingredient suppliers, wholesalers, and international distributors.
Food-grade ethanol should meet applicable purity, safety, and regulatory requirements for its intended use. Specifications, denaturant status, concentration, and documentation should always be confirmed before purchase.
Product Specifications
| Specification | Details |
|---|---|
| Product Name | Food Grade Ethanol |
| Chemical Name | Ethanol / Ethyl Alcohol |
| CAS Number | 64-17-5 |
| Chemical Formula | C₂H₅OH |
| Appearance | Clear, Colorless Liquid |
| Purity | Typically 96%–99.9% v/v, Depending on Grade |
| Odor | Characteristic Alcohol Odor |
| Water Content | According to Agreed Specification |
| Denatured | No — Food-Grade Supply |
| Heavy Metals | According to Applicable Standard |
| Methanol | Controlled According to Applicable Standard |
| Storage | Cool, Dry, Well-Ventilated and Approved Storage Area |
| Packaging | Drums, IBC Totes, Tankers or Bulk |
| Applications | Food Processing, Extracts, Flavors and Beverage Applications |
Final specifications, concentration, purity, packaging, certifications, and regulatory compliance should be confirmed according to the intended application and destination-country requirements.
High-Purity Ethanol
Food Grade Ethanol is valued for its purity and versatility. It can function as a solvent, extraction medium, processing ingredient, or formulation component depending on the specific food or beverage application.
High-purity ethanol is particularly useful where the presence of unwanted contaminants could affect product quality, flavor, aroma, or regulatory compliance.
Food and Beverage Applications
Flavor and Extract Production
Ethanol is widely used as an extraction medium for producing botanical extracts, flavor compounds, fragrances intended for food applications, and other specialty ingredients.
Food Processing
Food manufacturers may use ethanol in selected processing applications where food-grade alcohol is permitted and appropriate.
Beverage Manufacturing
Food-grade ethanol can be used in the production of alcoholic beverages and beverage formulations where permitted by applicable laws and regulations.
Natural Extracts
Ethanol can be used to extract compounds from herbs, spices, botanicals, and other approved raw materials.
Ingredient Formulation
Depending on the formulation and regulatory requirements, ethanol can serve as a carrier or solvent for certain food-grade ingredients and flavoring preparations.
Pharmaceutical and Related Applications
High-purity ethanol is also used as a processing solvent and ingredient in certain pharmaceutical, personal-care, and laboratory applications. However, the required grade and regulatory specifications may differ from food-grade requirements, so buyers should confirm that the product specification is appropriate for the intended application.
Quality and Purity Control
Quality control is essential for food-grade ethanol. Depending on the contracted specification, testing may cover ethanol concentration, water content, methanol, aldehydes, higher alcohols, acidity, residue, and other relevant parameters.
A Certificate of Analysis (COA) can be provided according to the applicable supply arrangement and product specification.
For international shipments, buyers may also request certificates or documentation relating to origin, quality, safety, and regulatory compliance.
Packaging Options
Food Grade Ethanol can be supplied in packaging formats appropriate for commercial transportation and storage, including:
- Drums
- IBC totes
- Tanker shipments
- Bulk quantities
- Other approved packaging by agreement
Packaging selection depends on order volume, transportation requirements, storage facilities, and destination regulations.
Storage and Handling
Ethanol is a flammable liquid and must be handled and stored using appropriate safety procedures.
It should be kept in approved containers and stored in a cool, well-ventilated area away from heat, sparks, flames, and incompatible materials. Appropriate fire-safety measures, ventilation, spill controls, and applicable hazardous-material handling procedures should be followed.
Storage and transportation must comply with applicable local and international regulations.
Why Choose Our Food Grade Ethanol?
- High-purity ethanol
- Clear and colorless liquid
- Suitable for approved food and beverage applications
- Suitable for flavor and extract production
- Food-grade, non-denatured supply
- Commercial quantities available
- Flexible packaging options
- COA and technical documentation available according to specification
- Suitable for international supply
- Suitable for food processors, beverage manufacturers, and ingredient distributors
Reliable Wholesale Ethanol Supply
Our Food Grade Ethanol is suitable for companies requiring a dependable supply of high-purity ethanol for approved food, beverage, extraction, and processing applications.
We work with buyers to establish purity, concentration, packaging, quantity, documentation, destination, inspection requirements, and delivery terms before shipment.
Order Food Grade Ethanol
Looking for high-purity Food Grade Ethanol for commercial or industrial food applications? Contact our sales team for current availability, pricing, purity specifications, packaging options, minimum order quantities, COA availability, and shipping information.
All orders should be supplied and used in accordance with applicable food, alcohol, hazardous-material, and import regulations in the destination market.
Related products

Grains

Grains
Fertilizer

Sugar
Sugar
Grains
Vegetable Oil